Transparent SLA parts in MPC12 Clear and Somos WaterClear Ultra 10122, polished or clear-coated to a water-clear finish at our workshop near Cambridge. ISO 9001 certified.
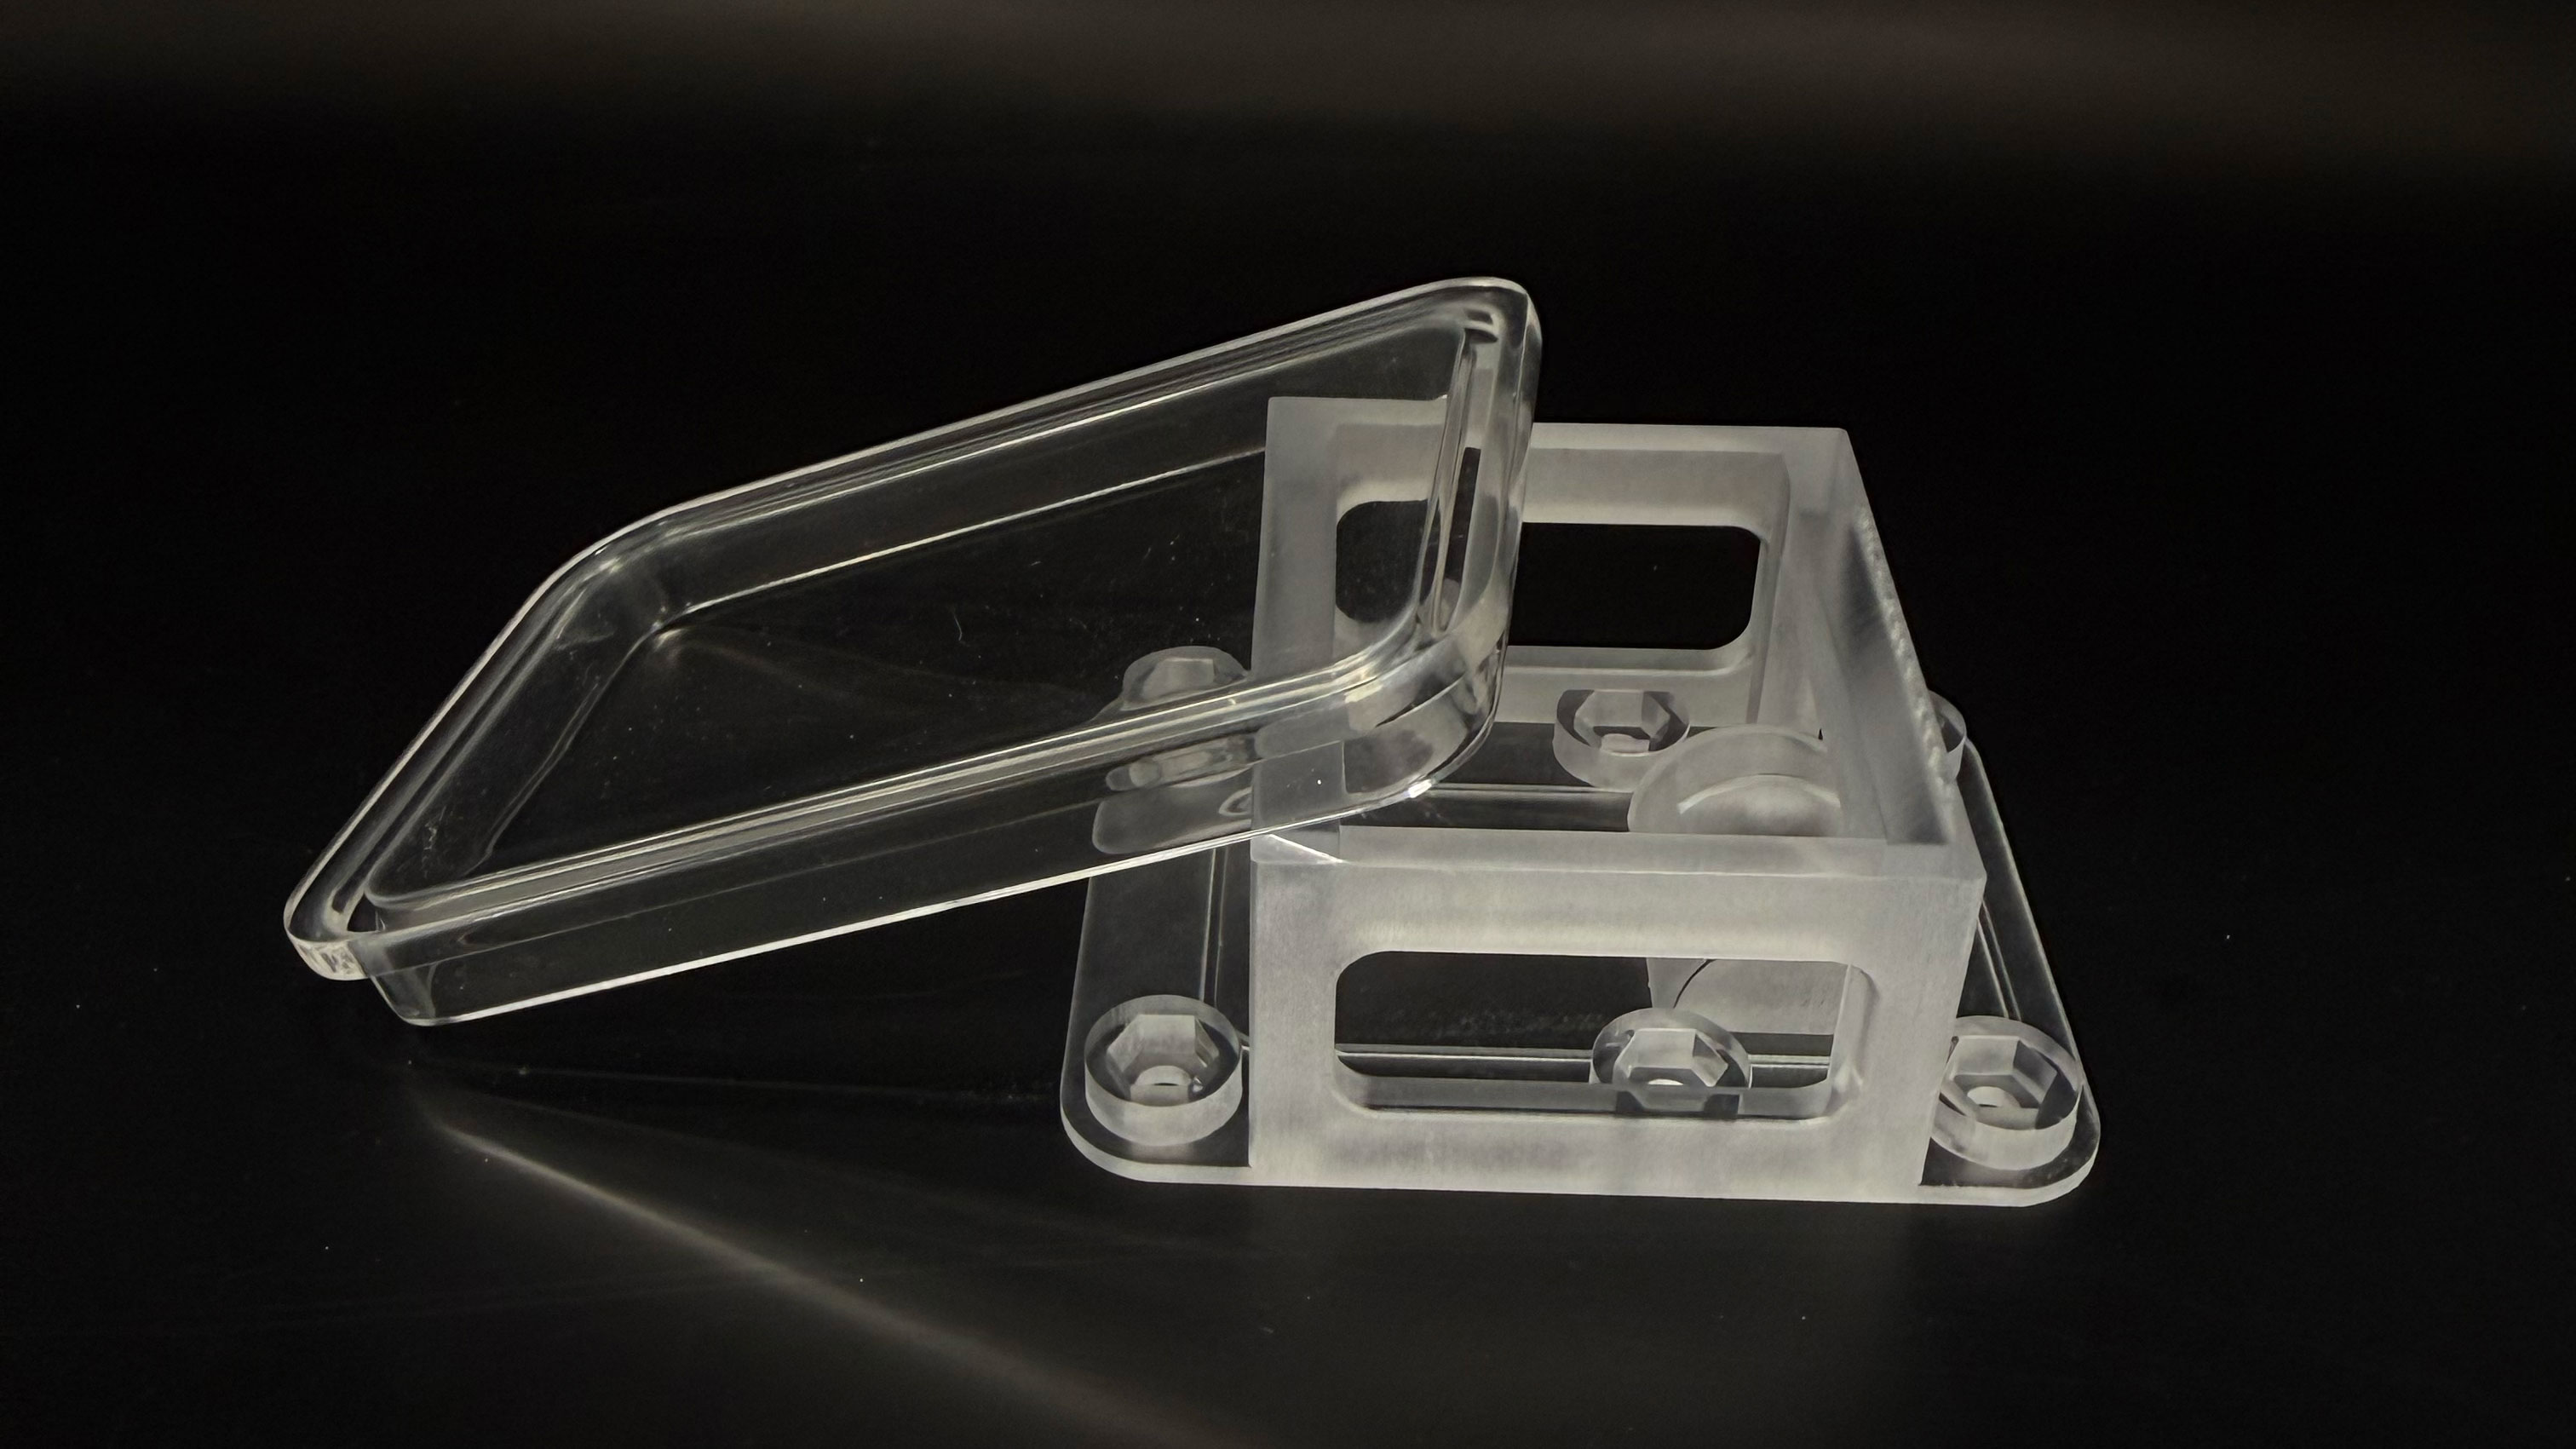
Complete Fabrication makes clear and transparent 3D printed parts using SLA (stereolithography) in two clear resins, Somos WaterClear Ultra 10122 and MPC12 Clear. Parts come off the machine translucent, so we finish them by polishing or clear-coating to a water-clear finish. Clear parts are used for light pipes, fluidics, see-through housings, lenses and display models. We have made prototypes in Whittlesford, near Cambridge, since 1986.
| Somos WaterClear Ultra 10122 | MPC12 Clear | |
|---|---|---|
| Best for | Light pipes, lenses, bottles and light transmission tests | Clear functional parts, flow visualisation, photo-elastic testing and casting patterns |
| Appearance | Optically clear, acrylic-like, refractive index 1.52 | Clear, multipurpose |
| Tensile strength | 56 MPa | 50 to 56 MPa |
| Elongation at break | 7.5% | 8 to 15% |
| Heat deflection temperature | 47 °C (0.46 MPa) | 49 °C (0.45 MPa) |
| Data sheet | Somos WaterClear Ultra 10122 | MPC12 Clear |
Figures are typical values from the manufacturers' data sheets, and are not a guarantee for a finished part.
SLA builds each part in thin layers, and the tiny steps between layers scatter light, so a clear print looks frosted straight off the machine. We remove those steps by polishing or clear-coating the surface, which gives a true water-clear finish. Polishing works best on faces we can reach, and clear-coating suits more complex shapes.
We can achieve good clarity with post-processing on any thickness, but thinner is better for a natural finish clarity. (Chris, 3D Print Department Manager)
For several identical clear parts, vacuum casting in clear polyurethane copies an SLA master, so parts come from one silicone mould instead of being finished one by one. We used this route for the I-Dration water bottle: we grew the bottle in two parts on our SLA machine, vacuum cast it in clear polyurethane and bonded the top and bottom for a watertight seal. For acrylic parts we use CNC machining, as we did for the full-size figures that hold our heart valve models. FDM 3D printing in PETG can give translucent parts, but SLA gives the clearer result.
CAD received by 5:30 pm is usually delivered the next day when capacity allows. Polishing to water-clear adds finishing time, which we confirm at quote. To quote your clear parts we need:
There is no minimum order. Send your brief to Info@compfab.co.uk, call +44 1223 836837, or use the contact page.
Yes. SLA 3D printing in a clear resin makes translucent parts, and polishing or clear-coating makes them water-clear.
Somos WaterClear Ultra 10122, an optically clear SLA resin with an acrylic-like appearance and a refractive index of 1.52.
Over time they can, especially in sunlight. For parts that must stay clear for years, we compare clear vacuum casting.
Only partly. We can polish faces we can reach, but internal channels stay as printed and look less clear.
Any thickness can be made clear with post-processing, but thinner walls give a more natural clear finish.
Usually when you need several identical clear parts, because the parts are cast from one silicone mould instead of being finished one by one.
Related:SLA 3D printing, vacuum casting, painting and finishing, materials and data sheets, 3D printing service and SLA batch production.