How to create 3D-printed medical prototypes in seven steps, from CAD export and process choice to biocompatible materials, sterilisation and moving to batches.
By Sebastian Stanley. First published 23 April 2025. Updated October 2026 by Tom Davies-Kent, Director, Complete Fabrication.
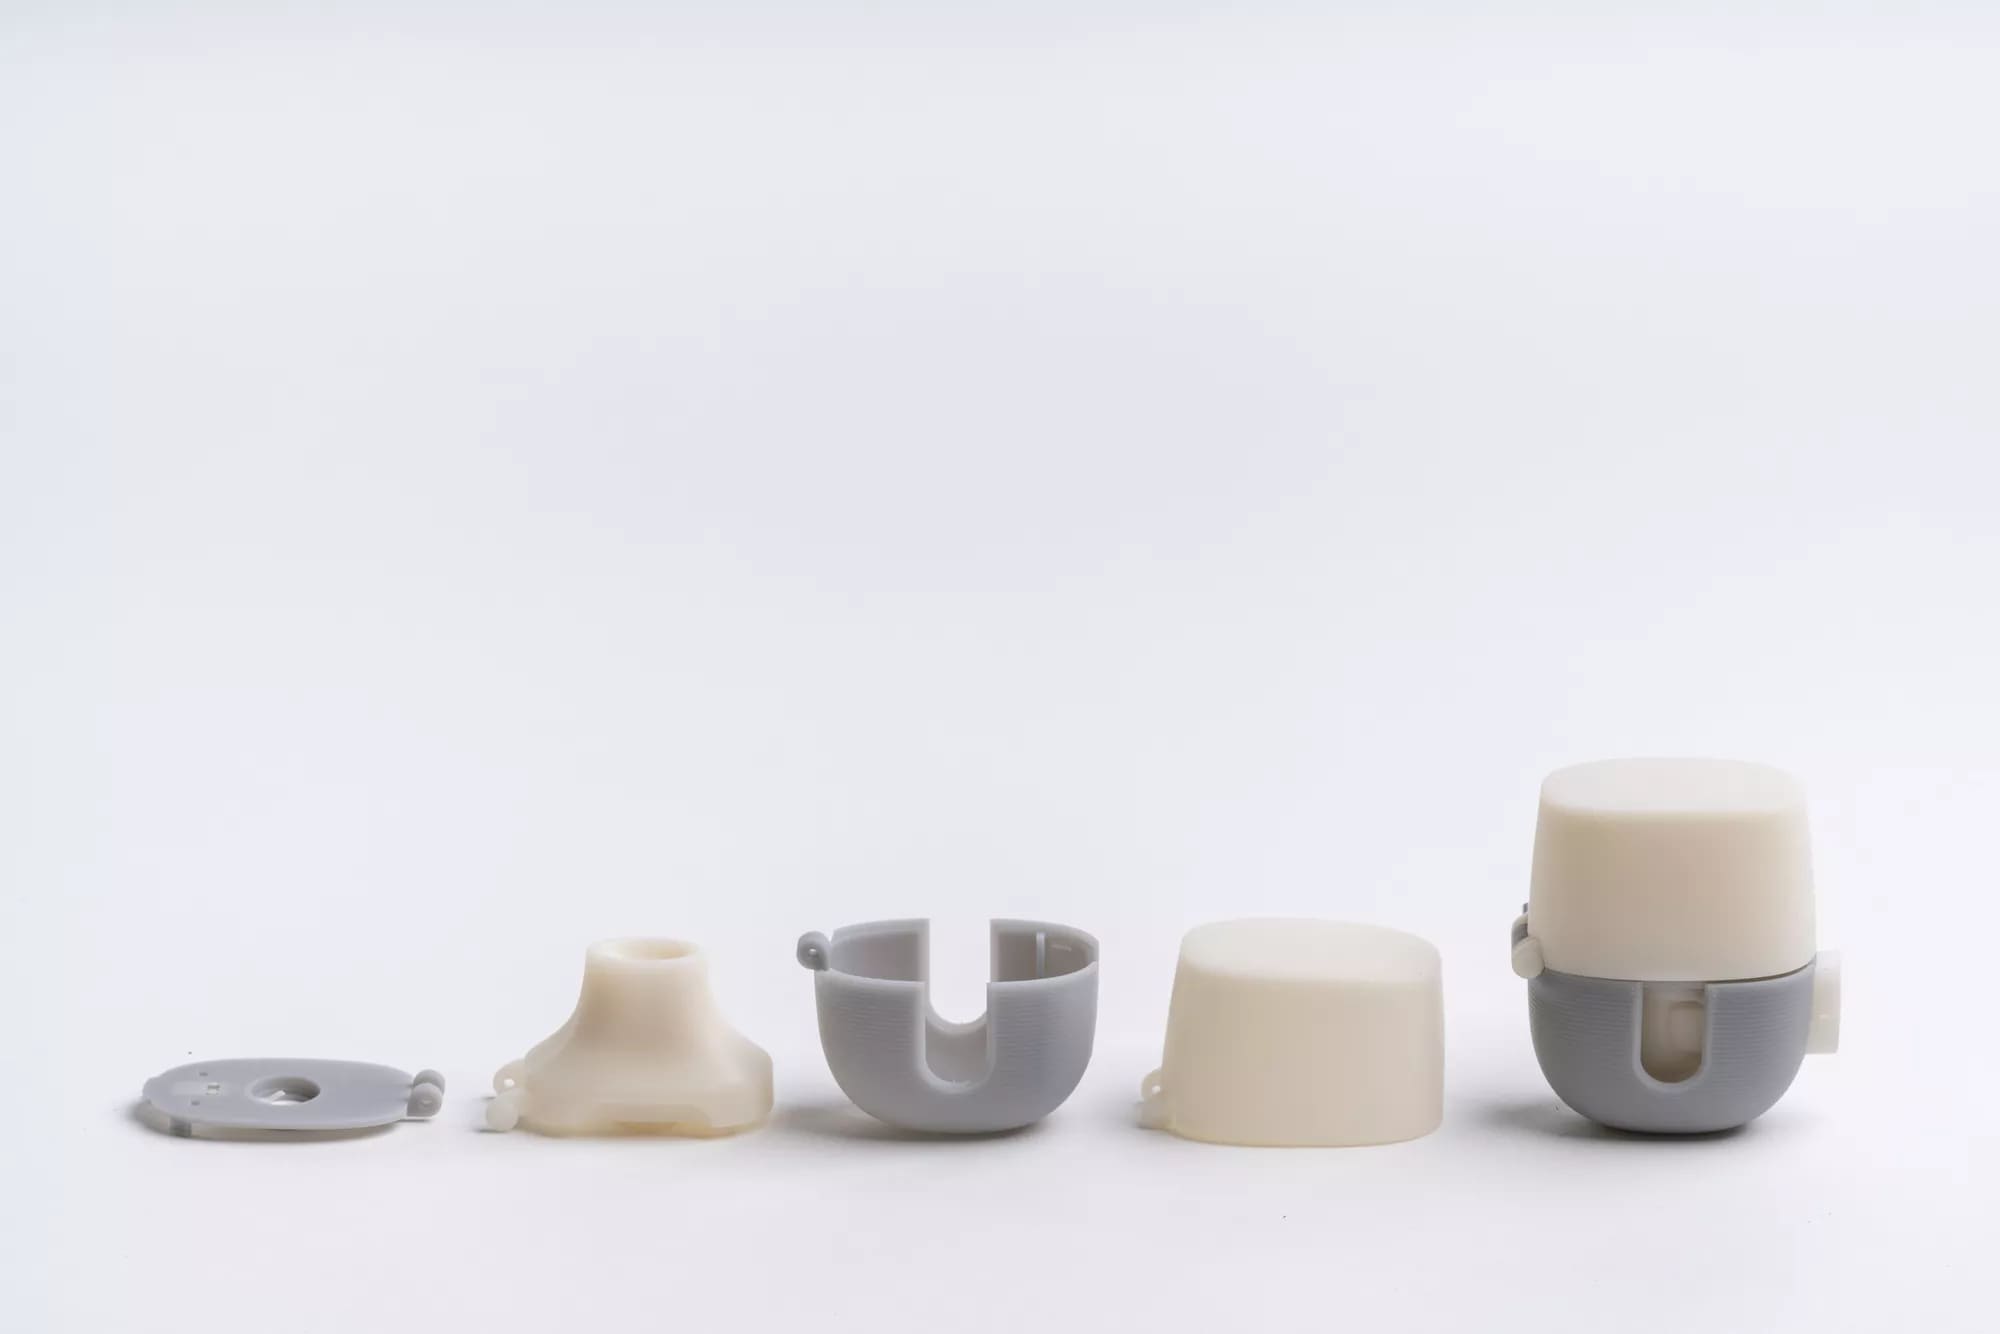
To create a 3D-printed medical prototype, decide what the prototype has to prove, prepare and export the CAD, choose the printing process and material, then finish, clean and test the parts. SLA holds about ±0.15 mm for detailed housings. Carbon DLS gives functional parts, including biocompatible grades. For batches of identical units, vacuum casting takes over.
Every prototype answers a question. Write it down before you print, because it decides the process, the material and the finish.
| If the prototype must… | It needs… | A good starting point |
|---|---|---|
| Show size, shape and grip | Accurate form and a realistic finish | SLA, sanded and painted |
| Test a mechanism or snap fit | Strength and repeatable dimensions | Carbon DLS or SLA in a tough resin |
| Touch skin in a user study | A material with biocompatibility data | Carbon MPU 100 or SIL 30 |
| Be handled by many users in a study | Tens of identical units | Vacuum casting from an SLA master |
| Test a clear fluid path or window | Optical clarity | Clear SLA resin, polished |
| Act as a large, simple fit-check model | Low cost and fast build | FDM |
A clinical review of 227 surgical papers found 3D printing in use for anatomical models, surgical guides and custom implants (Tack et al., 2016). Device prototypes are used earlier, to develop and test a product before it becomes a finished medical device. The steps below are the order we work through medical device plastic prototypes in our workshop.
Most 3D printing starts from a mesh. The CAD model is approximated by triangles, usually in an STL file, then sliced into layers (Wong and Hernandez, 2012). Coarse triangles show up as flats on curved faces, so export at a fine resolution.
We accept STEP, STL, IGES and SolidWorks files. STEP is the most useful, because we can check and adjust the solid model before we print. Before you send it:
Our SLA design guidance and design for manufacture guide cover the details.
The right process depends on the question from step 1. These are the routes we use for medical work, with the accuracy we hold.
| Process | Typical accuracy | Strengths for medical prototypes | Where it falls short |
|---|---|---|---|
| SLA (stereolithography) | ±0.15 mm | Fine detail, smooth surfaces, clear parts; 24-hour turnaround as standard | Standard resins are not for skin contact |
| Carbon DLS | Process-dependent; ask us | Functional parts with injection-moulding-like strength; certified biocompatible resins; batches of 1,000 small parts | Smaller build volume than SLA |
| FDM | ±0.4 mm | Low-cost, large, simple fit-check models | Visible layers; less detail |
| SLS and MJF (sourced through partners) | Varies by supplier | Tough nylon parts with no supports | We source these; we don't print them in-house |
| CNC machining | ±0.10 mm | Real engineering plastics and metals, including PEEK | Limited by tool access |
Many medical prototypes combine processes. A typical handheld device might have SLA housings, Carbon DLS internal parts and a CNC-machined metal component.
For a looks-like model, material choice is mostly about appearance. For anything that touches a patient or user, it is about biocompatibility.
Biocompatibility depends on the finished part as well as the resin. The printing process, washing, post-curing and finishing all affect the result. ISO 10993-1 sets out how to evaluate a material according to the type of body contact and its duration.
We run certified biocompatible materials on our Carbon DLS printers, including Carbon MPU 100 and SIL 30. We supply the material data you need for your own assessment. See all our materials and data sheets.
Our standard SLA finish is supports removed and bead blasted. Parts are washed in IPA and post-cured in a UV oven. From there, they can be sanded, painted, polished clear or textured to match a production finish. Painting or polishing adds at least a day.
Parts that clinicians will handle can be cleaned with medical-grade isopropanol wipes, or to a cleaning regime you specify.
Sterilisation needs care, because printed materials respond differently to each method. One study tested five 3D printing resins after low-temperature vaporised hydrogen peroxide sterilisation. Parts within a specific design window were sterile, and the materials showed no significant change in strength or dimensions (Eveland et al., 2024). Those results apply to the materials and designs tested. Check the data for your own material, part and sterilisation method before a study.
Test the prototype against the question from step 1, then change the design and print again. With fast turnaround, a change made in the morning can be a new part the next day, when capacity allows.
Involve users early. A review of medical device development found that capturing user requirements is an essential part of making safe, effective devices (Martin et al., 2008). Looks-like models in users' hands often reveal problems that never show up on screen.
Usability studies and clinical trials need identical units, often tens of them. At that point, single prints become slow and inconsistent, and the process changes:
We make the batch, check every unit and supply Certificates of Conformity for manufacture and materials when you flag the need at quote. See trial batches for how a batch runs.
3D printing is one part of the medical device prototyping process, which runs from concept to pilot builds. For the case for small batches, see the advantages of small-scale production for medical prototypes.
Examples from our workshop include the Piona self-injector, designed to look and feel like a beauty product, and the SAMBA II diagnostic instrument.
It depends on what the prototype must prove. SLA suits detailed housings and clear parts. Carbon DLS suits functional parts and offers certified biocompatible resins. FDM suits large, low-cost fit checks. For batches of identical units, vacuum casting is usually better than printing.
Only if they are made in a material with biocompatibility data and processed correctly. Standard SLA resins are not for skin contact. Carbon MPU 100 and SIL 30 are certified biocompatible materials, and the right choice depends on the type and duration of contact.
Some can. Results depend on the material, the part design and the sterilisation method. Studies have shown specific resins tolerating low-temperature hydrogen peroxide sterilisation, but check the data for your own material and method first.
STEP is best, because the solid model can be checked and adjusted before printing. We also accept STL, IGES and SolidWorks files. If you send STL, export it at a fine resolution so curved faces stay smooth.
SLA parts are ready in 24 hours as standard, and CAD received by 5:30 pm is usually delivered the next day when capacity allows. Painting or polishing adds at least a day. Batches get a firm lead time when we quote.
Send your CAD files and tell us what the prototype needs to prove. We will recommend a process and material, and confirm the cost and timeline. Call +44 1223 836837, email info@compfab.co.uk, or contact us.
Send your CAD files or drawings and tell us when you need the parts. Call +44 1223 836837 or email info@compfab.co.uk.
Contact us